Chemical Plant Automation Solutions | Process Control & Digital Transformation | ES&E - Electric Supply Equipment Co
Optimize Chemical Smart Manufacturing Automation
Chemical manufacturers face growing pressure to improve production efficiency, reduce operational costs, maintain strict safety standards, and minimize unplanned downtime—all while managing aging infrastructure and evolving market demands. Advanced chemical process automation and digital transformation technologies help modern chemical plants operate smarter, safer, and more efficiently through connected systems, real-time analytics, and intelligent asset lifecycle management.
Scale Operations with Advanced Chemical Process Control
Modernize and scale plant operations with intelligent automation platforms such as Rockwell Automation’s PlantPAx® distributed control system (DCS), designed specifically for process industries. Solutions like FactoryTalk® Batch and FactoryTalk® Analytics™ PavilionX™ support optimized batch processing, model predictive control (MPC), and advanced multivariable process optimization for greater stability, lower energy usage, and improved throughput.
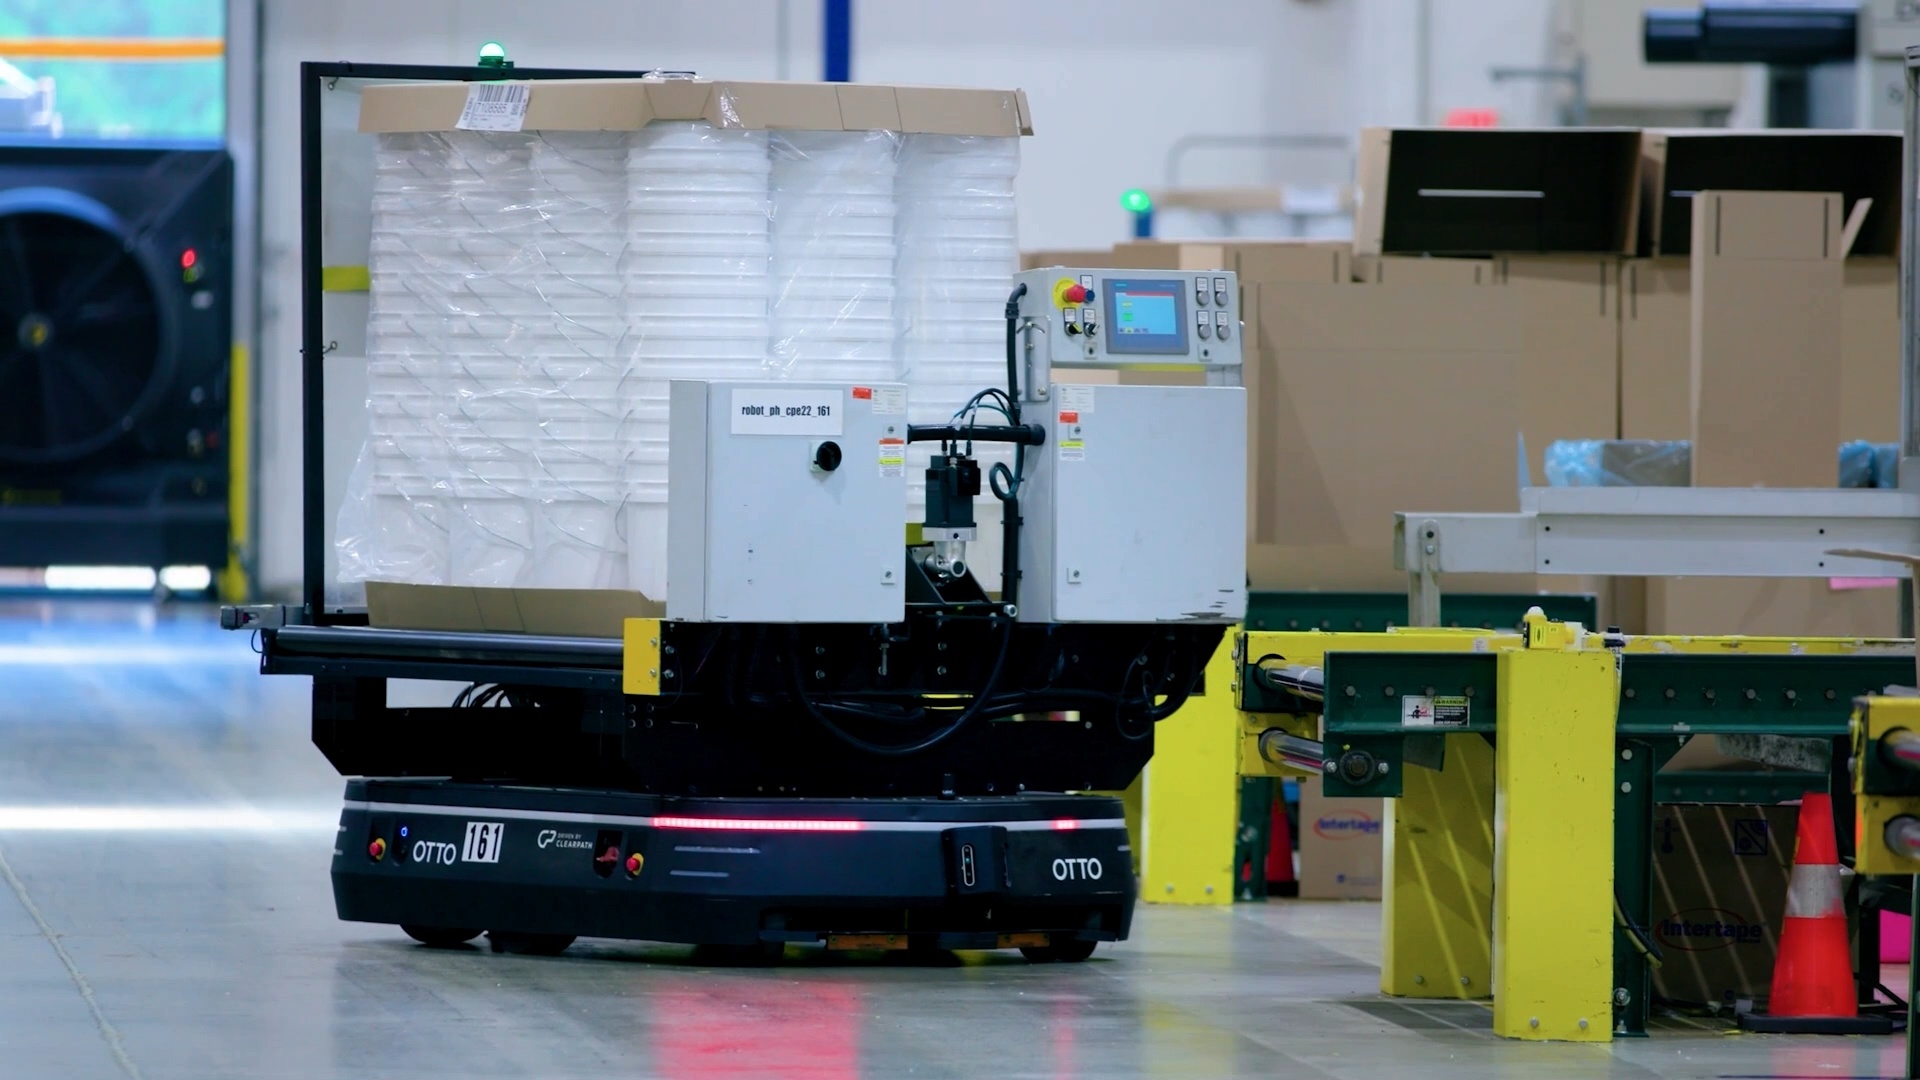
NEW OTTO Autonomous Mobile Robots (AMR)
Material Handling Built for Complex Facilities
- Production uninterrupted by labor gaps
- Flexibility for evolving manufacturing needs
- A breakthrough in efficiency
- Safety concerns put to rest
Narrow aisles, multiple shifts, and constantly changing workflows make manual material movement slow and error-prone. OTTO autonomous material handling solutions, including [AMRs / AGVs / autonomous forklifts], are configured around your facility's layout and processes. They reliably move materials between receiving, production, and shipping, cut manual touches, and help you reach higher efficiency targets without disrupting the operations you have in place.
Chemical Plant Automation & Digital Transformation Solutions |
Shop All Categories |
Strengthen Plant Safety, Modernization & Cybersecurity
Real-time equipment monitoring and predictive maintenance technologies enable proactive asset management to prevent unexpected failures before they occur. Modern chemical manufacturing requires secure, resilient operations. Aging infrastructure and legacy systems increase operational and cybersecurity risks that can impact safety, compliance, and productivity.
- Upgrade obsolete control systems and equipment
- Improve process safety with integrated safety instrumented systems (SIS)
- Protect critical infrastructure from cyber threats
- Maintain compliance with industry standards and regulations
- Future-proof operations with scalable automation technologies
Case Study
Advanced Analytics Improve Chemical Process Performance
FactoryTalk® Analytics™ Pavilion8® helped a chemical manufacturer optimize process performance, improve production stability, and increase operational efficiency. By leveraging model predictive control (MPC) and advanced analytics, the company reduced process variability, improved throughput, lowered energy consumption, and enhanced overall plant reliability through smarter, data-driven decision-making.
Case Study
Optimizing Power Generation with Smart Automation & Analytics
Advanced automation and digital optimization solutions improved power generation efficiency, reliability, and operational performance. By leveraging real-time monitoring, predictive analytics, and intelligent process control, the operation reduced downtime, optimized energy production, and enhanced overall asset performance—supporting more sustainable and cost-effective power generation operations.
Case Study
Plant-Wide Alignment Improves Operational Efficiency & Performance
How plant-wide alignment and connected automation technologies improved operational visibility, collaboration, and production efficiency. By integrating systems, standardizing processes, and leveraging real-time data insights, the organization enhanced decision-making, reduced inefficiencies, and optimized overall plant performance—creating a more agile and productive manufacturing environment.
Preferred Products
Rockwell Automation's components and systems deliver quality that you can depend on, giving you the freedom to focus on the task at hand. And by selecting from our wide range of preferred products, you can easily select the right products with high-availability to keep your operations moving.
With preferred products you get:
- Build with confidence — choose preferred products for reliable delivery and simplified selection
- Help reduce complexity and planning risk with our core architecture solutions
- Accelerate operations and improve schedule reliability with high-availability products
- Standardize globally, deliver locally